 Terms & Conditions
 Locations
Avoiding RCBO 40A Mis-Specification in Commercial Switchboards
Learn how to avoid costly protection mistakes by specifying the right RCBO 40 amp residual current protection for commercial switchboards and compliance.
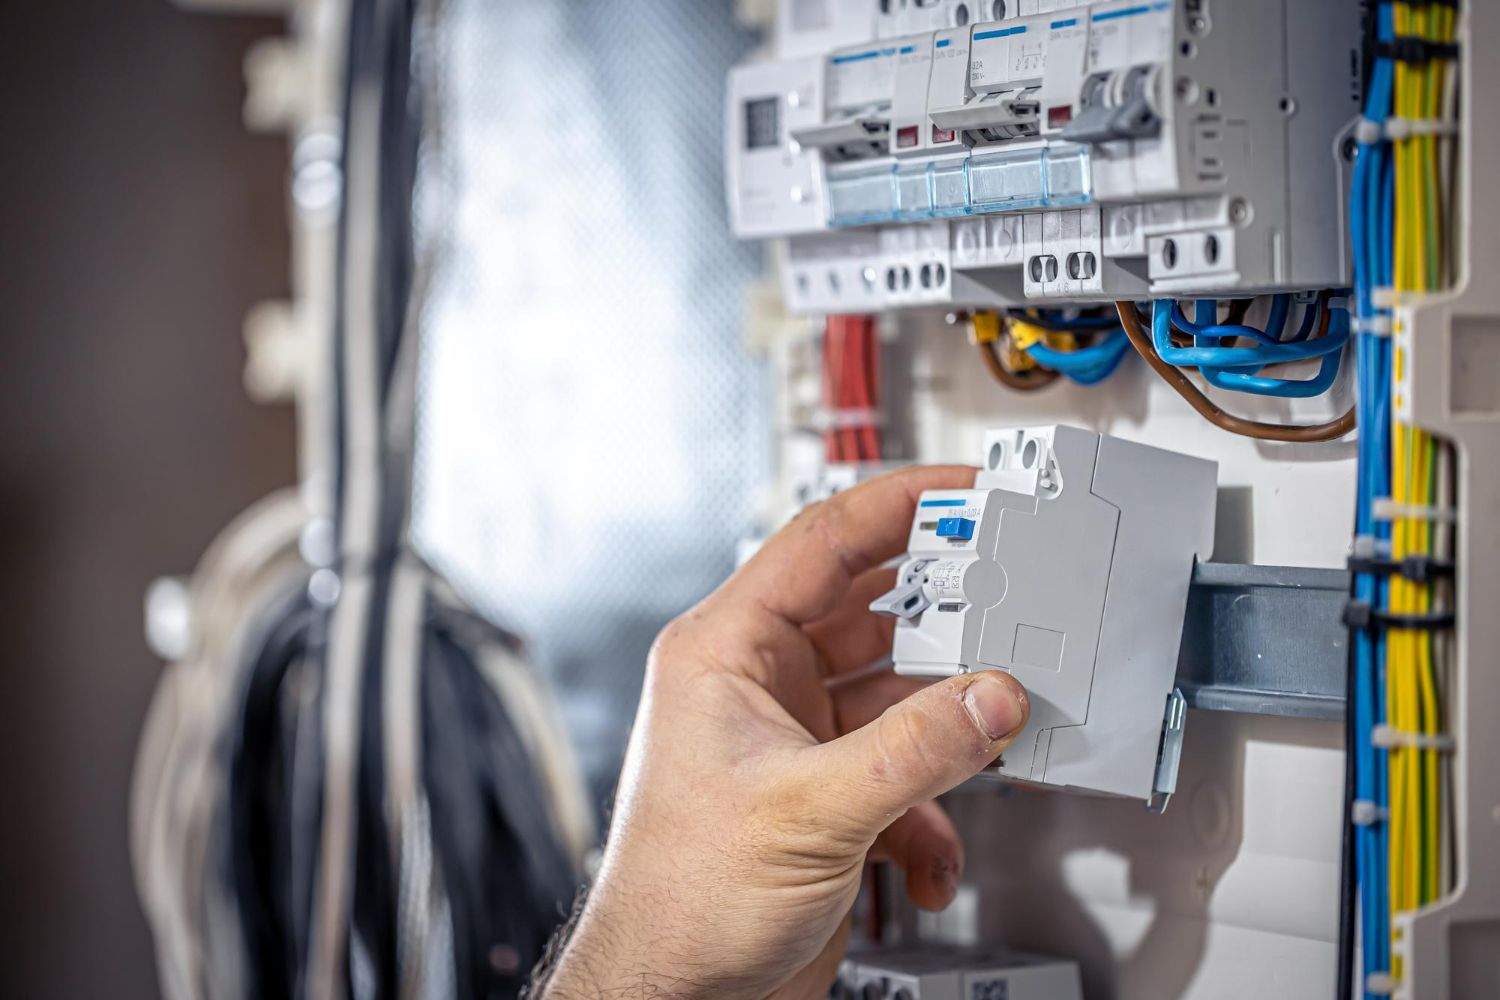
Industrial plants in Australia take a real hit once the late winter and early spring storms roll in. Lightning, strong winds and unstable supply can flip a smooth production day into a mess of trips, alarms and fault lights. Keeping lines running is not just about strong gear, it is about how well that gear is protected from sudden surges.
In factories, quarries, processing plants and commercial buildings, even one bad surge can stop everything. PLCs lock up, drives throw errors, power supplies die and protection devices trip out. That all leads to lost production and stressed maintenance teams trying to work out what failed first.
That is where Schneider Electric’s Acti9 surge protection range comes in, with the Acti9 iPRD surge arrester withdrawable cartridge sitting at the heart of the system. It gives a clear way to protect against surges and get power back online faster after a hit. As an Australian online supplier focused on Schneider Electric switchboard components, we work with electricians, OEMs and switchboard builders who want their boards ready for storm season, not scrambling after it.
On many Australian sites, surges do not only come from direct lightning strikes. They creep in from all kinds of everyday events, such as:
The scary part is that not every surge blows something up right away. A lot of the damage is slow and sneaky. Power supplies might keep running but run hotter. VSDs can show odd trips now and then. Control gear might reset once in a while, and it is easy to blame software or operators instead of the power quality feeding the panel.
Over time, those small surges stress insulation and electronic components. That turns into:
Because of this, good Type 2 surge protection at main and sub‑distribution boards is now seen as normal practice on serious industrial and commercial installations. It is not a fancy extra, it is part of good design, especially when the site has long cable runs, sensitive control systems or is in a storm‑prone area.
Schneider Electric’s Acti9 iPRD surge arrester withdrawable cartridge is built with day‑to‑day maintenance in mind, not just lab specs. The key features many electricians appreciate are:
Instead of having to disconnect wiring or replace a whole device after a major surge, you can pull the used cartridge, clip in a new one and move on. That means less time with covers off and fewer hands near live parts. For plants that run long hours, this can be the difference between a quick scheduled stop and a long unexpected shutdown.
Because the Acti9 system is widely used in Australian industrial and commercial switchboards, iPRD cartridges slot easily into many standard layouts. OEMs and switchboard builders can keep their designs consistent and straightforward. With the right selection, the Acti9 range also supports compliance with local wiring rules and good engineering practice for surge protection on important circuits.
Good surge defence starts at the drawing board. Where you place the Acti9 iPRD surge arrester withdrawable cartridge in a board has a big impact on how well the whole installation rides out a storm.
For most plants, that means protection at:
Multiple iPRD devices can be coordinated so that surges are controlled in stages. Upstream devices take the heavy hit, while downstream devices limit what actually reaches the most sensitive loads. Good discrimination with upstream breakers and fuses helps keep nuisance tripping to a minimum while still clearing real faults.
When choosing the right cartridge, designers and contractors should think about:
Switchboard builders also need to allow the space and layout to make cartridge changes easy. That means planning DIN rail positions, segregation, clear labelling and enough front access so that maintenance staff are not reaching awkwardly around other gear just to pull a cartridge. A little thought in the workshop can save a lot of time on site later.
Once the switchboard is in service, the value of the Acti9 iPRD surge arrester withdrawable cartridge really shows up in day‑to‑day maintenance. Visual status indicators make it simple for crews to check protection during regular inspections. If a cartridge shows it has taken a hit, it can be swapped as part of a planned shutdown, not in the middle of a crisis.
During storm season, when lightning and grid events are more common, this quick changeover becomes an uptime advantage. After a strong surge, maintenance teams can:
For OEMs, designing their machines and control panels with iPRD cartridges built in makes life easier for the end user too. Clear instructions can be given on how to check the devices and when to call an electrician to replace them. That helps lower the total cost of ownership across the life of the equipment.
Many plants choose to keep a small stock of spare cartridges on site. That way they are not waiting on freight at the worst possible time, like when a storm front has just rolled through and the plant needs to get back to full output.
Storms are part of life across much of Australia, especially from August onward when the weather starts to turn. Industrial sites that take surge protection seriously tend to have fewer unexplained shutdowns, fewer strange drive trips and less pressure on maintenance teams when the sky lights up.
Reviewing surge protection is not just about adding devices to a main board. It is about stepping through critical production lines, motor control centres and automation panels and asking where a surge could creep in and what it might damage. Electricians, OEMs and switchboard builders who make the Acti9 iPRD surge arrester withdrawable cartridge a standard part of their designs give themselves and their customers a clearer, safer and quicker way to stay protected.
At Switchboard in a Box, we focus on supplying Schneider Electric switchboard components, protection devices, motor control and automation hardware that fit how Australian sites really operate. When surge protection strategy, good switchboard design and smart maintenance planning all work together, plants are better prepared for whatever the next storm front brings.
If you are planning a new installation or upgrading an existing switchboard, we can help you select the right Acti9 iPRD surge arrester withdrawable cartridge for your project. At Switchboard in a Box, we work with you to ensure compliance, safety and ease of maintenance from the start. Speak with our team about your requirements and we will provide clear, practical advice. To discuss your project or request a quote, simply contact us.
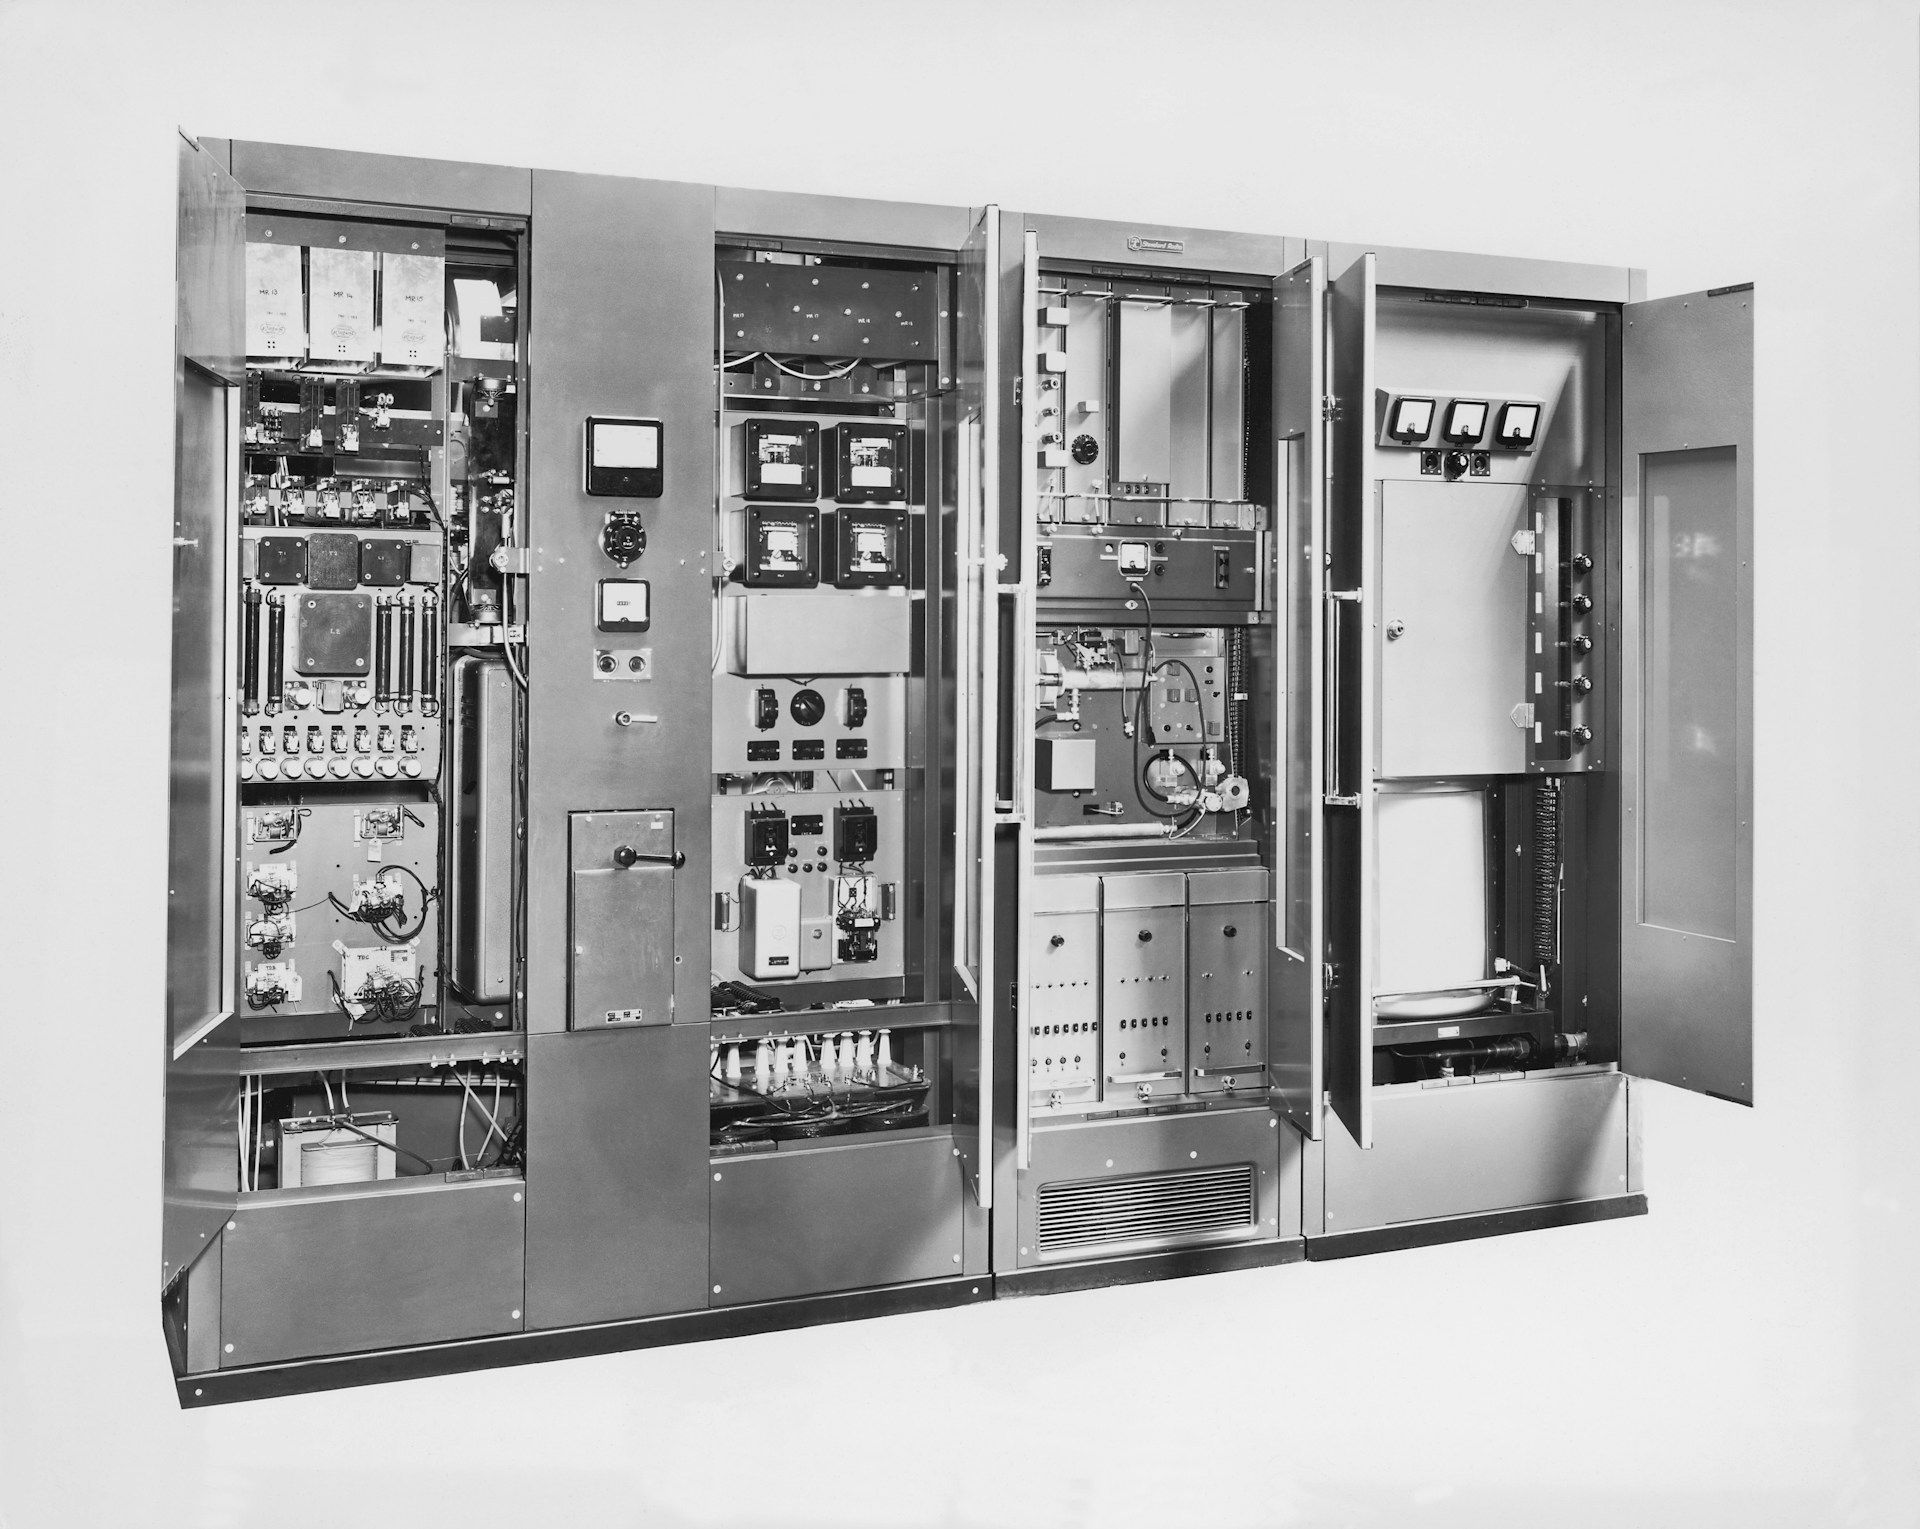
Many plants across Australia are stuck in the same spot: old motor control centres still running, but not running well. The drives trip too often, parts are hard to find, and no one really wants to plan a full MCC replacement that will shut things down for days.
Altivar 71 drives give another option. Instead of ripping out whole sections of a board, we can retrofit these drives into existing motor control panels and lift performance without a full redesign. It is a way to stretch the life of panels that still have good bones, while improving control, protection and reliability.
Late winter and August in particular are a smart time to think about this. There is still a bit of breathing room before the summer heat pushes cooling loads, pumps and process lines to their limits. Planning Altivar 71 upgrades now means your key motors are steady and ready when temperatures climb and demand peaks.
With the right planning, you can keep the gear you already know, avoid big rebuilds, and still get better drive performance where it matters most.
Not every panel needs new drives, but there are clear signs that an Altivar 71 swap is worth a serious look. We see the same triggers again and again in plants and facilities:
When these problems start stacking up, it helps to step back and look at a few decision factors before you commit to a full MCC rebuild.
Key things to review include:
Altivar 71 drives can be fitted as targeted replacements on those trouble spots. By picking off the worst performers first, you can smooth out problem areas, cut energy use on long-running loads like fans, and often delay a large MCC replacement for years. That frees up capital for other projects like new lines, safety upgrades or site expansions.
Before choosing any Altivar 71, the panel itself needs a proper check. A bit of upfront care here saves pain on site later.
On the power and installation side, make sure you are clear on:
Then look at how the control side is built today. Most existing panels have their own contactors, overloads and hardwired interlocks that you still want to use. Things to review include:
The Altivar 71 has flexible I/O and can usually sit neatly into this picture, but it is better to map it out on paper first.
Compliance and safety also matter. In Australia you need to be confident your upgraded panel will align with standards such as AS/NZS 3000 and AS 61439, along with any site rules. That includes checking short circuit ratings, correct earthing, EMC practices and safe lockout and tagout points so electrical work can be done safely during faults or shutdowns.
Altivar 71 drives have a wide feature set, but the real value comes from matching those features to what your motors actually do each day.
For different loads, you might focus on:
On the integration front, there are a few paths you can take. Many existing panels still run mostly on hardwired signals, and the Altivar 71 can work happily in that mode. Where plants are moving to digital networks, you can add communication options for Modbus, Profibus or Ethernet, and tie the drive into the site control system. The choice often comes down to what your PLC and network setup already look like.
Reliability and maintainability are where retrofit projects can quietly win. Some simple but important checks include:
Done well, your upgraded section should be easier to live with than the old gear, not just more complex.
In many parts of Australia, the pattern is pretty clear: winter is calmer, and summer is when systems get pushed. Using late winter and early spring for drive upgrades makes good sense, especially for cooling towers, building HVAC, irrigation, mine dewatering and other long run services.
Seasonal planning often works best when you:
Site readiness is just as important as the gear itself. Before anyone turns a screw, it helps to:
To reduce risk even more, many plants use staged changeovers. For example, you might:
That way, critical services stay available while new drives are integrated and proven inside the existing panels.
Aging motor control panels do not always need the scrap heap. With smart use of Altivar 71 drives, you can turn those panels into efficient, reliable and compliant parts of the plant again, without committing to full replacement.
A practical way forward is to:
At Switchboard in a Box, we work with Schneider Electric switchboards, switchgear, drives, motor control, protection and enclosures every day, supplying projects across Australia. Thoughtful planning, careful panel checks and well chosen Altivar 71 retrofits can keep your existing motor control panels working harder and smarter for many years to come.
If you are planning your next motor control upgrade or new installation, we can help you integrate the Altivar 71 into a practical, compliant solution. At Switchboard in a Box, we work with you to size, configure and package your drives so they are ready to install with minimal site work. Tell us about your project requirements and we will recommend a tailored approach that suits your budget and timeline. To discuss specifications or request a quote, simply contact us.